Environment Management & Mitigation Plan · Distilleries & Ethanol
Environment Management and Mitigation Plan for Distilleries
A distillery's Environment Management Plan has to convert the spent wash strategy into daily operating limits (storage days, concentration ratio, boiler feed and biogas utilisation) because that is the form in which it can actually be followed.
Screening view on your project, with the category and route named. No obligation.
What this means for distilleries & ethanol
The clearance is granted on a strategy; the plant runs on limits. An EMP that describes bio-methanation, evaporation and incineration in narrative terms tells an operator nothing about what to do at 2 a.m. when the digester is off-gas and the lagoon is filling. The version that works states the numbers: the maximum days of spent wash that may be held before production is curtailed, the concentration the evaporator must achieve for the boiler to fire the concentrate stably, the minimum biogas utilisation, the freeboard below which a lagoon may not be filled, the condensate quality required before reuse, and the ash quantity to be lifted per period. These are operating limits with consequences attached, and they are also exactly what the half-yearly compliance report is later assembled from.
How KIPL runs it
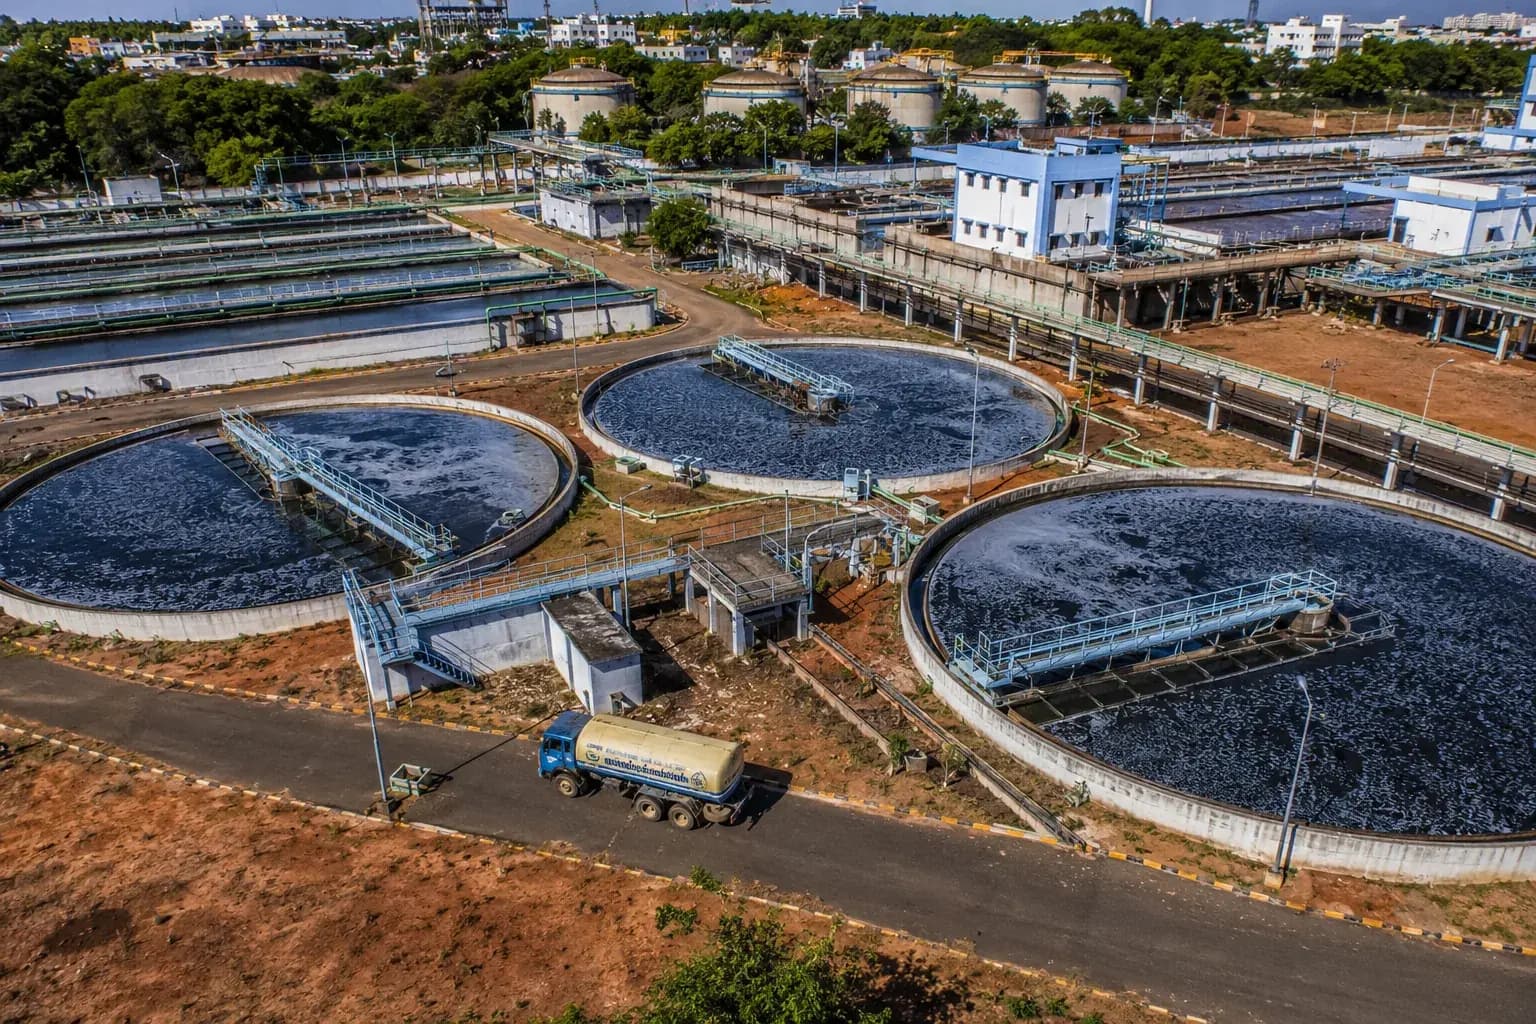
Around the effluent core sits the rest of what a distillery's neighbours actually experience. Odour is the dominant social impact and it has identifiable sources (open lagoons, digester vents, molasses storage, the fermentation section) each of which needs a specific control rather than a general commitment. Boiler emissions, ash storage clear of rainfall and wind, and the groundwater monitoring network around storage complete the plan. KIPL writes each measure with a number, an owner and a record, so it can be implemented by the plant and evidenced by it. What goes wrong otherwise is an EMP that reads well and cannot be operated: no stated point at which accumulating spent wash requires production to slow, and therefore no point at which anyone does.
- EC conditions
The EMP becomes enforceable
Mitigation committed in the EMP is written into the clearance and consent and reported half-yearly, so limits stated vaguely become limits that cannot be demonstrated.
- Storage cap
Holding days are the operating constraint
Because lagoon storage is permitted as a volume and a holding period, the EMP must state at what inventory production is curtailed rather than allowing accumulation to continue.
- Odour
The neighbours' issue is the plan's issue
Odour from lagoons, digester vents, molasses storage and fermentation is what the public hearing raised, so the EMP has to name each source and its control.
What you receive
Written for distilleries & ethanol, not adapted from a template.
- 01Spent wash operating limits: maximum holding days, lagoon freeboard, and the inventory trigger at which production is curtailed
- 02Evaporator concentration duty and boiler feed specification, with the minimum concentrate solids for stable firing
- 03Biogas recovery and utilisation targets, with flaring or venting treated as a reportable exception
- 04Source-wise odour control plan for lagoons, digester vents, molasses storage and the fermentation section
- 05Ash handling plan: quantity, covered storage, and the utilisation or disposal route
- 06Groundwater monitoring network around storage, boiler and ambient monitoring schedule, budgets and a responsibility matrix
Questions from distilleries & ethanol
What distilleries & ethanol ask before appointing us.
Answered against the regulation as it stands, not as a sales pitch. If your situation is not here, ask us directly.
Ask a question →Why does the EMP need to state storage days as a limit?
Because storage is the only buffer in a distillery's effluent system and it is finite. Without a stated inventory at which production is curtailed, the plant continues distilling through a digester or evaporator outage and the lagoon fills past its permitted holding, which is a consent and clearance breach that the EMP could have prevented by naming the trigger.
How is odour controlled at a distillery?
Source by source: covering or minimising open lagoon surface, capturing and utilising digester gas rather than venting it, managing molasses storage, and containing the fermentation section. A single general commitment to control odour cannot be audited, and it does not answer the specific complaint the surrounding villages made.
What happens to the biogas?
It is normally used as boiler fuel, which offsets fossil fuel consumption and is one of the few genuinely favourable numbers in a distillery's environmental case. The EMP should set a utilisation target and treat flaring or venting as an exception to be recorded, because unrecorded venting is both a lost benefit and an odour source.
Does the EMP cover the ash from the incineration boiler?
It should. Firing concentrated spent wash produces a potash-rich ash in quantities that need covered storage and a defined utilisation or disposal route. Ash left in the open is a recurring inspection finding, and it is an avoidable one if the EMP fixes the lifting frequency and the storage arrangement.
Who implements the EMP once the plant is running?
The plant, through named responsibilities against each limit. The reason for writing it this way is practical: the half-yearly compliance report is assembled from the records those responsibilities generate, and an EMP without owners produces no records to assemble.
Can the EMP be revised as the plant learns to operate?
Tightening a control or adopting a better measure than the one committed is straightforward and should be reported. Relaxing a committed limit is a different matter, because the limit is part of what the clearance was granted on, and changing it is a matter for the authority rather than for the plant.
Stage by stage
How environment management & mitigation plan actually runs, step by step.
Also for distilleries & ethanol
The rest of the environmental brief for this sector.
Relevant proof
EIA for Synthetic Organic Chemical Industry
CTE/CTO application, ToR application, baseline data collection, EIA report and appraisal before the EAC: Category 5(f), the sector KIPL holds Category A accreditation in.
- Capacity
- 20 → 140 TPM
- 5(f) accredited
- Cat A
Where we do this
Environment Management & Mitigation Plan for distilleries & ethanol, city by city.
Other sectors
Who else we run environment management & mitigation plan for.
Next step
Tell us the project, and we will tell you the category and the route.
Screening is the cheapest stage to get right and the most expensive to get wrong. We will say plainly what environment management & mitigation plan your distilleries & ethanol project needs, and what it does not.
Start the conversation